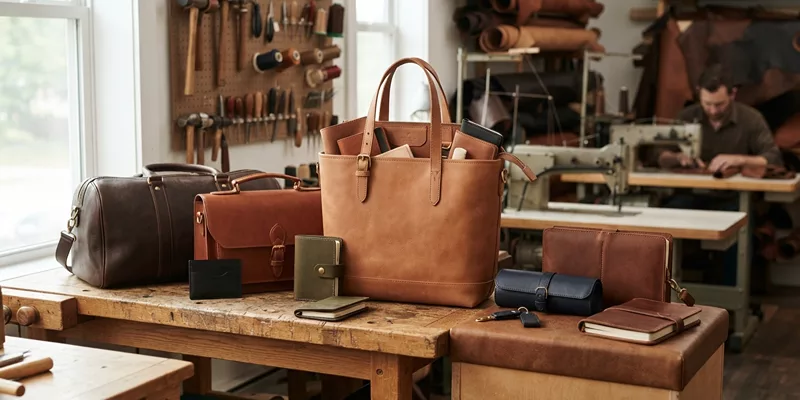
Five leather samples arrived from the brand's previous vendor in one envelope, and in the photographs they were indistinguishable.
On the bench, two days into the audit, they were not: the grain wandered across paired panels, the edge paint chipped under a thumbnail and the zipper travelled with no resistance at all.
That gap between a picture and a hide is what the brand had been paying 12% defects for.
The rebuild replaced appearance as an acceptance test with a written spec — grade, tannery, panel symmetry, hardware, edge finish — and by the end of the fourth month the final 5,000-unit run closed at zero critical defects with margin up 18%.
Why the Samples Passed and the Bags Failed
The vendor met the brief closely enough to keep winning the order. Where it failed was at the points a photograph cannot show.
Grain that wanders
Two panels cut from different parts of a corrected hide never match in daylight, and the mismatch only reads once the bag is assembled.
Edge paint with no bite
Paint that has not bonded to the grain peels in flakes along the strap edges, and it peels first where a hand grips.
Hardware without weight
Light plated clasps and loose zipper pulls feel thin in the hand and wear through their finish inside a season.
"Genuine leather" as a spec
The words name neither a grade, nor a tannery, nor an acceptable variance, so nothing on the purchase order can be failed.
Audits read as guarantees
A tannery's environmental certification says nothing about the finish, the panel yield or the hardware on the assembled bag.
Inspection without a rule
When the acceptance test is "looks right", the decision moves to a junior buyer thousands of miles from the bench.
Quality Inspector Chen ran the first check on the bench rather than on paper. A standard mechanical pass — forty handle pulls and a rub test — lifted the edge paint on the commodity sample almost immediately, and the plating on the clasps had already dulled where the hardware rubbed itself.
The thickness of the failure was the useful part: it was not a factory that could not make a bag, but one that had never been told what to fail on.
So the work split into a material decision and a rules decision, and the rest of this record takes them in order.
What followed was one rule set: a hides-and-hardware spec with written variance limits, and an inspection flow applied the same way to all lots.
Performance Specs in Place of Appearance
The change started with the bill of materials. Production Manager Li replaced the word “luxury” with thresholds a bench inspector could check under a lamp: leather grade, tannery consistency, panel yield and hardware durability.
Teardown Beside a Known-Good Piece
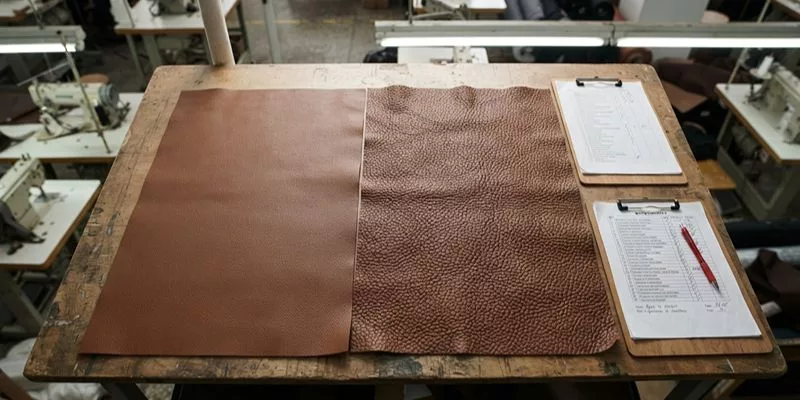
I laid the commodity bag next to the production candidate and worked through it with Technician Wang. The commodity hide showed uneven grain and shallow fibre density; the candidate held uniform grain across the sheet.
Edge paint on the commodity sample chipped under light pressure, while the candidate's edge survived a thumbnail without marking.
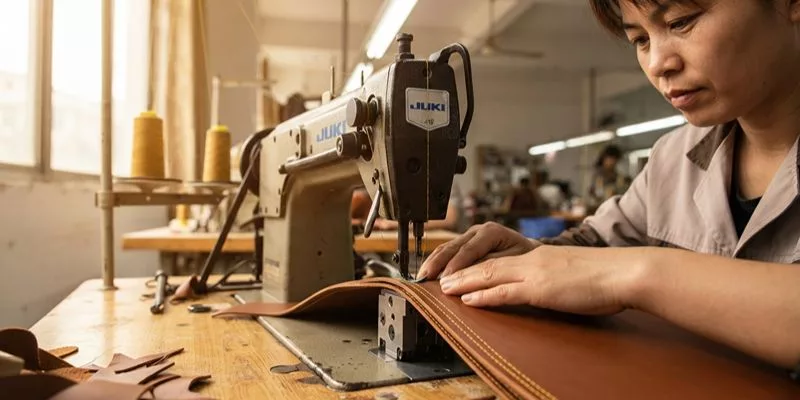
On the Juki 1541, stitch consistency separated them just as cleanly: the commodity panels slipped time and again, and the candidate held a steady eight stitches per inch.
A Material Report With Prices
Margins are set by the hide, so the choice was written down instead of argued.
I compiled the options against cost per square foot, observed defect risk and how the hide paired with available hardware.
| Hide option | Cost / sq ft | Defect risk | Verdict |
|---|---|---|---|
| Pigmented split | $1.80 | Finish peeling; scratches light plating | Rejected |
| Chrome-tanned top | $3.50 | Grain variance, controlled by mapping | Approved with QC |
| Veg-tanned full grain | $6.20 | Low, but needs heavy tooling | Held for next season |
Chrome-tanned leather brings softness and colour range, and it also brings chemical obligations under REACH that have to be documented rather than assumed.
Yvonne Cai, senior mechanical testing and leather finishing manager, signed off the second tannery only after the grain pattern held steady across cut panels.
The upgrade added $1.10 to the landed unit cost, taken deliberately because a bag that peels costs more in returns than the hide costs to buy.
The Inspection Flow, Locked Before Cutting
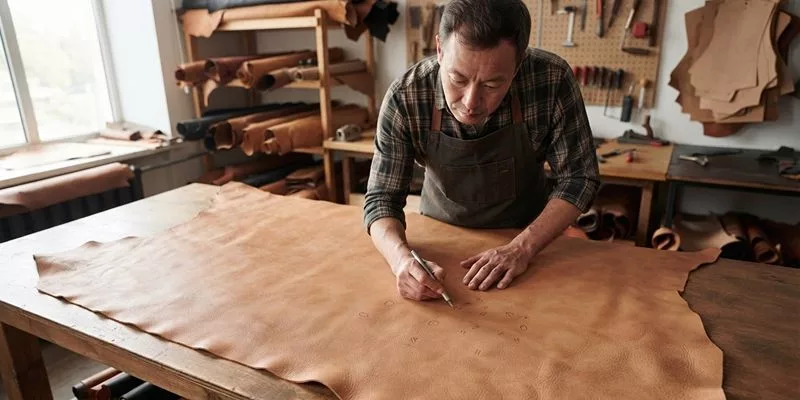
With the material set, the same steps were applied to all lots in the same order, so a defect could be stopped where it began rather than sorted at the dock.
- Incoming hide checkInspector Chen compares grade, thickness and finish against the approved swatch.
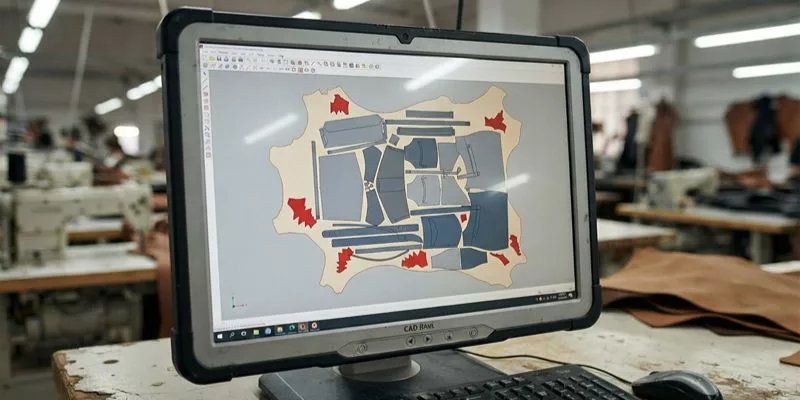
- Hide grading and mappingCutter Zhang marks out scars and reserves clean areas for the visible panels.
- Hardware inspectionPlating consistency, zipper travel and mould match are checked against the signed sample.
- Pre-production lockThe bill of materials, stitch targets and measurements are frozen before bulk cutting starts.
- In-line checksStitch density and glue marks are corrected at the machine, not after assembly.
- Durability testingEdge-paint adhesion and abrasion tests are run on hardware pulled at random.
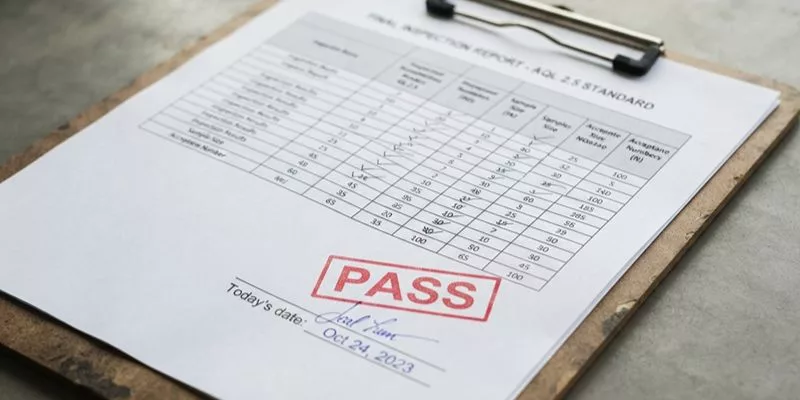
- Final random inspectionPacked goods are drawn by lot under AQL 2.5 and passed, reworked or held.
Pass and Fail, Written in Plain English
AQL only works when a defect is defined before it appears.
Grain misalignment across paired panels became a major defect, because it reads as two different bags on one shelf. Plating peel, a broken clasp and a weak rivet became critical defects, with no tolerance.
Only slight natural marks outside the focal area count as minor, and then only if the approved standard allows them.
| Defect | Class | Action |
|---|---|---|
| Grain mismatch on paired panels | Major | Panel re-cut before assembly |
| Edge paint lifting at the bend | Major | Lot held for re-finishing |
| Plating peel or broken clasp | Critical | Batch stopped, hardware rejected |
| Stitch density off target | Major | Machine re-set, panels re-run |
| Natural mark outside the focal area | Minor | Accepted under the signed standard |
Hardware Terms Spelled Out Up Front
Custom plates and pulls carry a mould fee, and the fee is where arguments begin later.
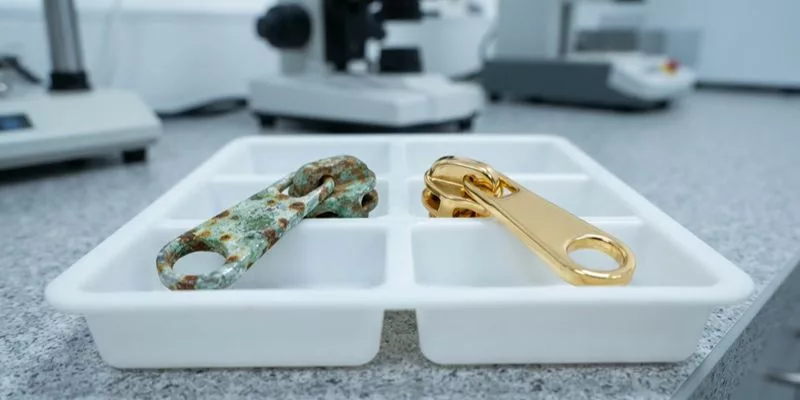
Hardware Technician Lin set the terms before the client approved a drawing: the mould cost is quoted separately, ownership is stated in writing, and premium plates require salt-spray evidence from the supplier before the run is released.
Her own salt-spray test on the client's original zippers had rusted the plating inside 48 hours — cheap hardware does not fail slowly.
The brand’s original samples had passed a visual inspection and then failed a bench test within minutes, which is the whole argument for writing the test down.
Two of the five came from tanneries whose leather was fine but whose grading scattered the clean panels across hides, and no photograph exposes that.
“A hide is not uniform, and pretending otherwise is where yields go wrong. Grade it, map it, and cut the visible panels from the cleanest section — the cost is in the layout, not in buying a more expensive sheet.”
Cutter Zhang, hide gradingWhat the Rules Changed
Four months after the first spec sheet, the floor was running a fixed flow and the numbers followed it rather than the other way round.
The 5,000-unit bulk run was drawn by lot under ISO 2859-1 at AQL 2.5.
The packed-goods log recorded zero mismatched panels, zero loose hardware and zero finish failures at the loading dock, so the critical defect rate closed at zero against a 12% starting point.
Sample approval dropped to 14 days, down from 45, because the pass/fail rules were written down before the first swatch was cut.
Quality Inspector Chen, final lot verification| Measure | Before | After |
|---|---|---|
| Critical defect rate | 12% across five samples | 0% on 5,000 units |
| Gross margin | Baseline, with trapped stock | +18% |
| Sample approval | 45 days of rework | 14 days |
| Edge paint | Chipped at 40 handle pulls | Held through abrasion test |
The gain reached the people who had to live with the old process. Founders got a launch date they could plan around; procurement had documented logic to show an internal approval board; a remote QA team could reject a panel on a written rule instead of a gut feel.
At the end of the final pack-out, QC Manager Lin noticed the floor change most clearly at the cutting table: the team stopped second-guessing the hides and simply matched the panel to the approved master swatch, which halved the daily inspection time.
“Once the grain rule was posted, nobody argued about a cut. The master swatch decided it, and the assembly line moved on to the next bag.”
Lin, Wuhan QC ManagerKey Takeaways on Private Label Leather
The file that made this work is short, and none of it is about aesthetics.
Approve hides, not labels
"Genuine leather" is not a specification.
Approve a tannery and a grade, then test how consistently that combination cuts into usable panels — a cheap hide with poor yield is the expensive one.
Treat hardware as a system
Plating, zipper travel and mould accuracy fail together.
Ask for salt-spray evidence and a written mould-ownership term before any tooling fee is paid.
Define the defect before the lot
A written classification moves the pass/fail decision onto the bench.
A junior inspector needs a rule, not an opinion, and the ISO sampling standard only bites once the classes are named.
Pay for the panel a customer sees
The hide upgrade cost $1.10 a unit and protected the retail price.
Visible leather carries the brand, so the cleanest section belongs on the panels a customer holds.
Ask for five samples from the same order rather than one.
A single bag shows what a bench can do; five show what a production line will repeat.
Future Outlook: Applying the File Elsewhere
The brand is now extending the same acceptance rules to a canvas collection, using the checklist Chen prepared for the leather lots.
That is the useful part of a documented flow: once grain, hardware and edge rules exist in writing, a new material only needs its own thresholds, not a new argument. A second SKU can be added on the same inspection logic and the same sample gate.
Methodology note: this record draws on live sourcing decisions, bench inspections and the final sampling review. I am not paid by any tannery or hardware supplier, and the test equipment used here is bought by the lab.